Ask an experienced slitting line operator what causes most recoiling problems, and the answer is often a single word: tension. Loose wraps, telescoped coils, strips that wander on the recoiler, edge damage and even surface marks can usually be traced back to how tension was created and controlled between the slitter head and the recoiler.
This article explains slitting line tension control: why slit strips need tension, why they do not all behave the same way, and how loop pits, tension units and recoiler drives work together. It is a process explainer for production teams and engineers. Specific settings depend on the material, thickness, width and line configuration, and should come from the equipment manufacturer and trials on your own material.
Why Slit Strips Need Tension
A recoiler cannot wind a tight, stable coil from slack strip. Each wrap needs to be pulled firmly against the one below it so the finished coil holds its shape during handling, packing and transport. Tension does that work. Too little, and the coil is loose and may telescope or collapse. Too much, and the strip can stretch, edges can be damaged, and soft or coated surfaces can be marked.
The challenge on a slitting line is that tension has to be applied to many strips at once, all wound onto the same recoiler mandrel.
Why Strips Wind at Different Rates
Master coils are rarely perfectly uniform in thickness across their width. Many have a slightly thicker centre than edges, a profile known as crown. When the coil is slit, strips from the centre are slightly thicker than strips from the edges.
On a common recoiler mandrel, all strips turn at the same rotational speed. The thicker strips build diameter faster and therefore take up more length per revolution. The thinner strips build diameter more slowly and take up less. Unless something compensates, the thinner strips go slack while the thicker ones stay tight. A US patent on tensioning metallic strips on a slitting line describes exactly this problem in its background: edge strips from a crowned sheet run slack while centre strips stay taut, and the slack has to be accommodated somewhere upstream.
That is why slitting lines use a combination of a loop and a tension unit before the recoiler.
The Loop: Storing the Difference
A loop gives the strips somewhere to hang between two parts of the line, so small differences in length can be absorbed rather than forcing every strip to run at exactly the same tension.
Loop pit
The most common arrangement is a pit in the floor between the slitter head and the tension unit. The slit strips hang down into the pit in a catenary. Strips that are running longer simply hang lower. Loop pits require civil work and add to foundation cost, which is why some lines use other arrangements.
Loop bridge or above-floor loop
Some lines use an above-floor loop or a loop table instead of a pit, depending on material thickness and the plant’s civil constraints. Heavy-gauge lines may also have a loop before the slitter head to separate the decoiler from the slitting section. Valgo’s published heavy gauge slitting line configuration, for example, lists a first loop after the uncoiler and straightener and a second loop ahead of the tension unit.
Loop control
The depth of the loop is usually monitored by sensors so the line can adjust speeds to keep the loop within limits. A loop that runs too deep or too shallow is a sign that upstream and downstream speeds are not balanced.
The Tension Unit: Creating Back Tension
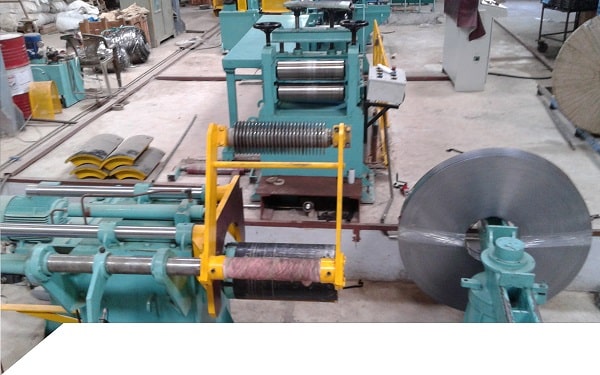
After the loop, the strips pass through a tension unit, sometimes called a tension stand. Its job is to hold the strips back so the recoiler has something to pull against. Several approaches are used:
Friction pad tensioners
The strips pass between pads, often lined with felt or another friction material, which are pressed together. Pressure on the pads sets the drag. This approach is common and relatively simple. Pad material and condition matter: worn or contaminated pads can mark the surface or give uneven tension.
Roll-type tensioners
Here the strips wrap around a set of rolls whose rotation is resisted by a brake or drive. Because the strip is not dragged across a stationary surface, roll tensioners are often used where surface quality is important.
Belt and other designs
Belt-type and combined designs are also used, particularly for sensitive surfaces or specific materials. The right choice depends on material, thickness, surface finish and line speed.
The Recoiler: Turning Tension into a Tight Coil
The recoiler pulls the strips through the tension unit and winds them. Its drive control has to account for the coil diameter growing from the mandrel to the full outside diameter. As diameter increases, the same tension requires more torque at lower speed. Modern recoilers use drive control to manage this so tension stays reasonably consistent through the coil.
Before the recoiler, a separator, typically an arbor with separator discs, keeps the slit strips apart so their edges do not interleave or rub as they wind. An overarm separator or pressure arm may also be used to help keep the strips tracking correctly.
Common Tension-Related Problems
- Loose or soft coils: Insufficient back tension, worn pads, or a recoiler drive not compensating for diameter
- Telescoping: Uneven tension across strips, misaligned strips or variations in strip thickness
- Strip breaks or edge damage: Excessive tension, particularly on narrow or thin strips
- Surface marks: Contaminated or worn pads, or the wrong tensioner type for the surface
- Strips wandering on the recoiler: Poor separation, uneven loop or misalignment between units
Tension problems can also look like other faults. Camber and edge quality issues may originate at the slitter head rather than in tension, so diagnosis should look at the whole line.
How Material Changes the Picture
Tension that suits one material can be wrong for another. Thin, soft materials such as aluminium need lower and more carefully controlled tension than heavier carbon steel. Coated or polished surfaces need tensioning methods that avoid marking. Heavier gauges need more powerful tension units and drives. We discussed aluminium-specific issues in Aluminium Coil Slitting: Challenges and Machine Requirements.
What to Discuss When Specifying a Line
- Thinnest and thickest material, and the full width range
- Surface finish and coating sensitivity
- Expected crown and thickness variation in incoming coils
- Narrowest strip width and maximum number of strips
- Maximum recoiled coil diameter and weight
- Available space and civil constraints for a loop pit
- Preferred tension unit type and how tension will be adjusted
Conclusion
Tension control is what turns a set of freshly slit strips into a set of tight, stable coils. The loop absorbs length differences between strips, the tension unit creates the back tension the recoiler needs, and the recoiler drive keeps it consistent as the coil grows. When each part is suited to the material and set up correctly, the result is a coil that holds its shape all the way to the customer.
Valgo designs Metal Slitting Line configurations, including light gauge slitting lines, around each customer’s material and finished-strip requirements. Contact Valgo Group to discuss a slitting process for your application.
